
Preventing cross-contamination in pharmaceutical storage facilities requires a combination of physical segregation, controlled environmental conditions, validated cleaning procedures, and strict inventory management protocols. No single measure is sufficient on its own: effective contamination control depends on layered defenses that together protect product integrity and patient safety. The sections below address the most important questions facility managers and engineers face when designing or operating a compliant pharmaceutical storage environment.
What are the most common sources of cross-contamination in pharmaceutical storage?
The most common sources of cross-contamination in pharmaceutical storage are shared handling equipment, inadequate physical separation between product categories, airborne particulate transfer, and human movement between storage zones. Contamination can originate from materials, surfaces, personnel, or airflows, and can be chemical, microbiological, or particulate in nature.
In practice, the risk is highest at transition points: where products move between zones, where equipment is shared without validated cleaning, or where high-potency, allergenic, or temperature-sensitive products are stored alongside general inventory without adequate barriers. Personnel who move between areas without following appropriate gowning or hygiene procedures introduce another well-documented contamination pathway.
Packaging failures, damaged totes or containers, and poorly maintained storage surfaces also contribute. In high-SKU environments such as pharmaceutical wholesale or distribution, the sheer volume and variety of products in close proximity amplify the risk, particularly when slower-moving or long-tail inventory shares space with faster-moving stock and receives less frequent inspection.
How does physical segregation prevent cross-contamination in drug storage?
Physical segregation prevents cross-contamination in pharmaceutical storage by creating defined boundaries between incompatible products, categories, or risk levels. Dedicated storage zones, physical barriers, separate racking systems, and controlled access points ensure that products with different contamination risk profiles do not share surfaces, airspace, or handling pathways.
Effective segregation operates at several levels. At the facility level, distinct areas are designated for quarantine, approved stock, rejected materials, returns, and high-risk product categories such as cytotoxics, narcotics, or allergens. At the storage unit level, dedicated totes, containers, or shelving prevent direct product contact between categories.
Access control reinforces physical segregation. Restricting personnel movement between zones, using color-coded equipment, and labeling zones clearly reduces the likelihood that human activity bypasses physical barriers. Quarantine areas deserve particular attention: products awaiting quality release must be unambiguously separated from approved inventory, whether through locked cages, dedicated rooms, or clearly marked and access-controlled zones within an automated system.
In high-density automated environments, segregation can be enforced at the software level as well, by assigning specific storage locations or totes to defined product categories and preventing the system from co-locating incompatible items. This adds a reliable, auditable layer of control that complements physical infrastructure.
What GMP requirements apply to pharmaceutical storage segregation?
Good Manufacturing Practice (GMP) and Good Distribution Practice (GDP) guidelines require that pharmaceutical storage facilities maintain clearly defined, separated areas for different product categories, control access to those areas, and document all storage and handling activities to support traceability and audit readiness. The specific requirements are set out in regional and international guidelines, including EU GDP guidelines and ICH Q10.
Key GMP storage requirements relevant to segregation include:
- Defined storage zones: Separate areas for quarantined, approved, rejected, returned, and recalled products, with unambiguous identification of each zone’s status.
- Temperature and environmental monitoring: Storage conditions must be validated and continuously monitored, with records available for inspection.
- Access control: Unauthorized personnel must be prevented from entering storage areas; access logs support audit trails.
- Batch traceability: Every product movement must be traceable by batch, lot number, and expiry date to support recall management and FEFO (First Expired, First Out) compliance.
- Handling of high-risk materials: Cytotoxics, narcotics, controlled substances, allergens, and highly active materials require dedicated storage with additional physical and procedural controls.
- Documentation and SOPs: All segregation procedures must be defined in validated standard operating procedures and supported by training records.
It is important to note that compliance is a property of the complete implementation, not of any single piece of equipment or infrastructure. Hardware, software, validated procedures, environmental controls, and personnel training together determine whether a facility meets GMP or GDP requirements. Automated storage systems can support compliant workflows, but formal compliance status depends on the entire validated system.
How do HVAC and airflow design reduce contamination risk in pharma warehouses?
HVAC and airflow design reduce contamination risk in pharmaceutical warehouses by controlling the movement of airborne particles, maintaining appropriate temperature and humidity, and creating pressure differentials that prevent contaminated air from migrating between zones. Properly designed airflow is one of the most effective passive contamination controls available.
Pressure cascades are a central design principle. Areas with higher contamination risk are maintained at lower air pressure relative to adjacent clean zones, so that airflow moves away from sensitive product areas rather than toward them. This is particularly important where high-potency or allergenic products are stored, as airborne transfer of even trace quantities can represent a serious risk.
Temperature and humidity control protect product stability and reduce microbiological growth risk. Pharmaceutical products frequently have defined storage conditions (ambient, refrigerated, or frozen), and HVAC systems must maintain these conditions reliably across the entire storage volume, not just at monitoring points. Mapping studies are typically required to demonstrate uniform conditions throughout the storage area.
Filtration quality matters as well. HEPA filtration is standard in manufacturing environments and may be specified for certain pharmaceutical storage areas depending on the products handled. Regular filter maintenance, validated change intervals, and documented monitoring programs are necessary to sustain filtration performance over time.
In large automated storage structures, airflow design must account for the physical obstruction created by dense racking. Engineers should verify that HVAC modeling reflects the actual installed layout, since standard room-level calculations may underestimate temperature variation within a densely packed storage system that utilizes full building height.
What cleaning and decontamination protocols are required for pharmaceutical storage areas?
Pharmaceutical storage areas require validated cleaning and decontamination protocols that define the cleaning agents used, application methods, contact times, frequencies, and verification steps for each surface type and zone. Protocols must be documented, approved, and followed consistently, with records retained to support GMP audit requirements.
A compliant cleaning program typically covers the following elements:
- Cleaning agent selection: Agents must be appropriate for the surfaces being cleaned, effective against the contamination types present, and compatible with pharmaceutical product categories stored in the area. Rotation of disinfectants is often required to prevent microbial resistance.
- Written procedures: Each cleaning task must have a defined SOP specifying sequence, method, dilution, contact time, and rinsing requirements where applicable.
- Frequency schedules: Routine cleaning, periodic deep cleaning, and event-triggered decontamination (for example, following a spill, product failure, or pest incident) must each be scheduled and documented.
- Verification and monitoring: Swab sampling, visual inspection, or other verification methods confirm that cleaning has been effective. Results must be recorded and reviewed.
- Spillage procedures: Dedicated protocols for immediate containment and decontamination of spills, particularly for high-risk materials, are a regulatory expectation.
- Training records: Personnel carrying out cleaning must be trained on the relevant procedures, with training documented and periodically refreshed.
In automated storage environments, cleaning protocols must address both the open floor areas accessible to personnel and the interior of the storage structure itself. Totes used to carry pharmaceutical products should be subject to their own cleaning validation, defining how and when they are cleaned, inspected, and returned to service.
How does automated storage technology support contamination control in pharmaceutical facilities?
Automated storage technology supports contamination control in pharmaceutical facilities by reducing human movement through storage areas, enforcing software-controlled inventory segregation, enabling full batch and lot traceability, and presenting products to operators at controlled workstations rather than requiring personnel to navigate open storage aisles.
Fewer people moving through storage zones directly reduces the risk of cross-contamination from personnel. In a Goods-to-Person model, operators remain at defined workstations while the automated system retrieves the required tote. This concentrates human activity at a small number of controlled points, making it easier to enforce hygiene, gowning, and verification procedures consistently.
Software-controlled inventory management adds a reliable layer of segregation that physical barriers alone cannot achieve. An automated system with appropriate inventory logic can enforce FEFO retrieval, maintain batch separation, flag expiry dates, and prevent incompatible products from being co-located, providing an auditable record of every storage and retrieval event. This level of traceability supports recall management and regulatory inspection readiness.
Direct-access architectures, where every storage location is individually retrievable without moving other products, are particularly relevant in pharmaceutical environments. Systems that require digging or reshuffling inventory to reach a requested product create additional handling events, each of which introduces contamination risk and complicates batch traceability.
How Hexxabotics supports pharmaceutical contamination control
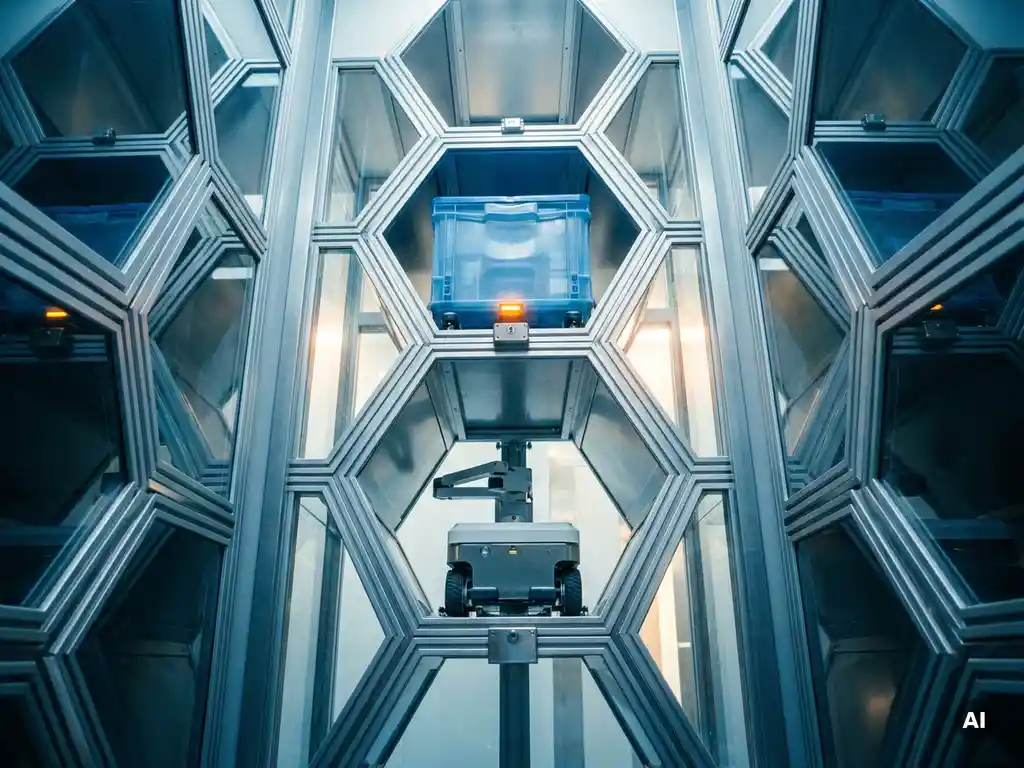
Hexxabotics provides a high-density, direct-access AS/RS designed to support the strict inventory control and traceability requirements of pharmaceutical storage and distribution. Key capabilities relevant to contamination control include:
- 100% direct access: Every tote is individually retrievable without digging or reshuffling, reducing unnecessary handling and supporting clean, traceable inventory movements.
- Batch and lot traceability: The system supports batch-controlled inventory workflows, enabling FEFO retrieval logic and audit-ready movement records when integrated with appropriate software.
- Goods-to-Person operation: Operators work at defined workstations rather than walking through storage aisles, concentrating human activity at controlled points and reducing cross-contamination risk from personnel movement.
- Software-enforced segregation: Inventory logic can separate product categories, quarantine zones, and batch groups within the same physical structure, enforcing rules that physical barriers alone cannot reliably maintain.
- Scalable architecture: Storage capacity and throughput scale independently, allowing pharmaceutical distributors to grow SKU counts or transaction volumes without redesigning the core infrastructure.
Compliance with GMP or GDP requirements depends on the complete validated implementation, including software, procedures, environmental controls, and customer processes. Hexxabotics is designed to support regulated pharmaceutical workflows and batch traceability as part of a properly validated system. To explore how the technology fits your specific pharmaceutical storage environment, contact the Hexxabotics team for a project-specific consultation.
Related Articles
- What technology is used for real-time pharmaceutical inventory monitoring?
- What is direct-access storage and how does it support drug recalls?
- How do you design a warehouse layout that supports multiple shifts?
- How does fleet management work for warehouse robots?
- What is swarm robotics and how is it used in logistics?